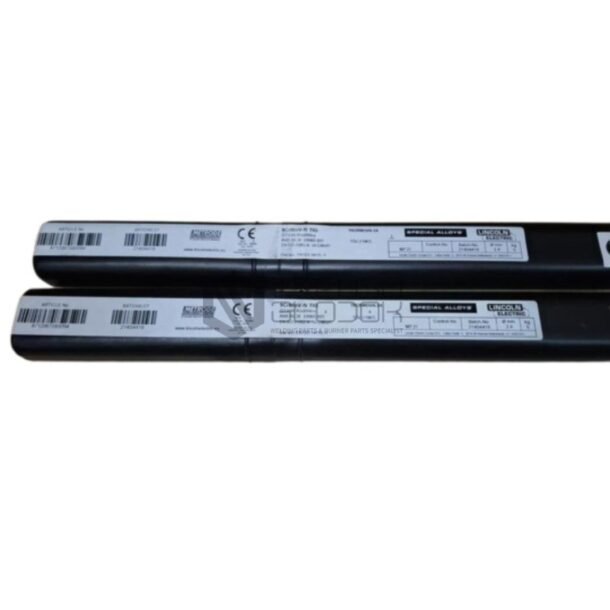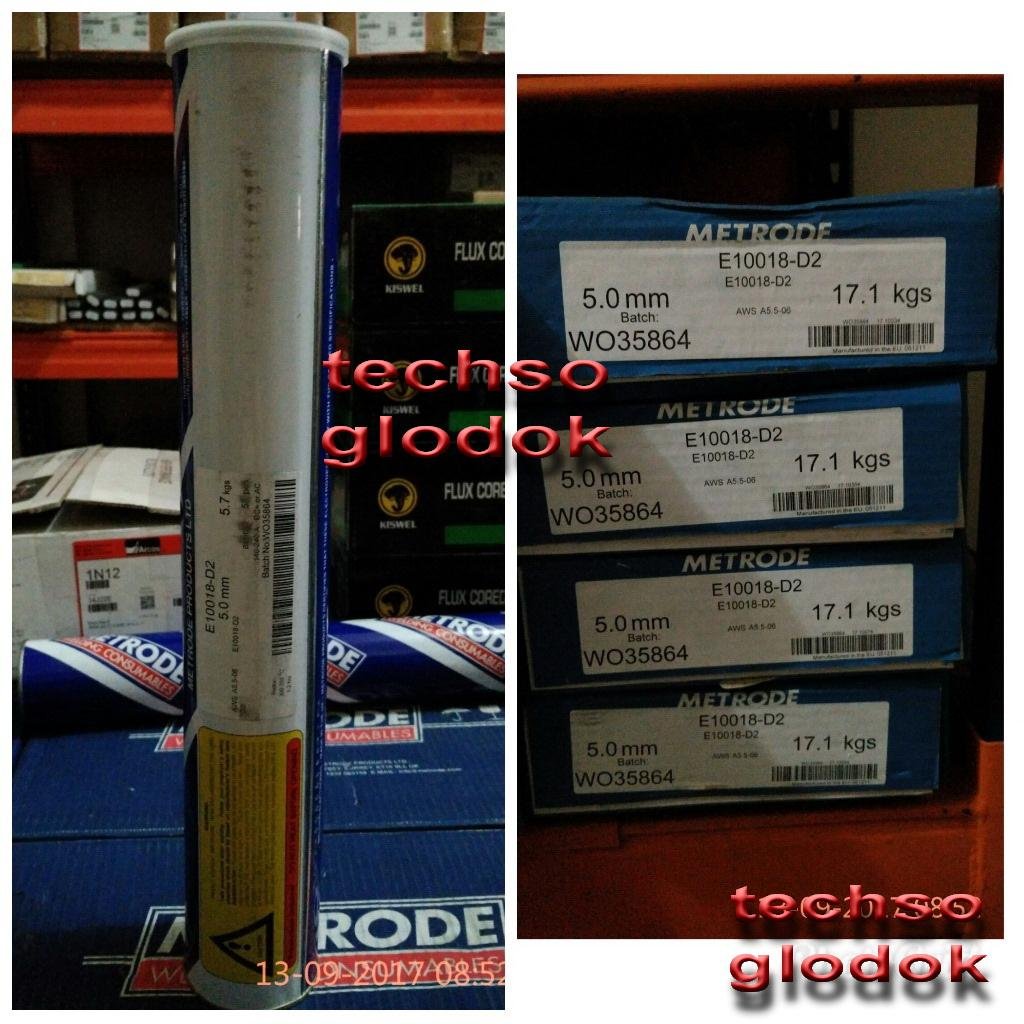
Metrode E10018-D2 dia 5.0 mm
Merek : Metrode
aws : E10018-D2
Dia : 5.0 mm
berat : 5,7 kg/can
MnMo HIGH STRENGTH STEELS
Alloy type
Low alloy steel consumables with MnMo additions for welding high strength steels.
Materials to be welded
These consumables are used for a variety of ferriticCMn and low alloy steels.
E9018-D1 is used formaterials with aminimum tensile strength requirement of 620MPa (90ksi); eg.AISI 4130 (90ksi condition), ASTM A487 grades 2A, B & C (cast).
E10018-D2 is used for materials with a minimum tensile strength requirement of 690MPa (100ksi); eg.
AISI 4130, 4140, 8630; BS970 grades 709M40 (En19); DIN 42CrMo4 (1.7225), 34CrMo4 (1.7220); ASTM A487 grades 4B, 4D & 6A (cast).
Applications
Fabrication of higher strength steels for use in the stress relieved condition. For offshore oil well-head process pipework and fittings, these low nickel consumables satisfy NACE MR0175 requirements intended to ensure resistance to sulphide-induced stress corrosion cracking in sour
service, combined with good sub-zero toughness. Also finds applications for the repair of medium
strength low alloy steel castings where a stress-relief only (rather than N+T) is to be applied.
Microstructure
In the stress relieved condition the microstructure consists of tempered bainite.
Welding guidelines
The actual preheat and PWHT requirements will depend on the base material being welded. Normally preheat/interpass temperatures will be in the range 100-250C.
PWHT
The PWHT requirements will depend on a number of factors including, basematerial, property requirements, need to conform to NACE etc. Temperatures will normally be about 620C but when welding 4130 using E10018-D2 temperatures up to about 645C may be
required to temper the HAZ.
Additional information
Although MnMo wire is the nearest match to the E9018-D1/E10018-D2 electrodes in terms of
composition when welding base materials requiring high temperature or prolonged soak PWHT (eg. 4130) it may